inquiry
Leave Your Message
0%

Hey there! You know, the construction and home improvement market is really booming right now, and people are on the lookout for some cool, sustainable materials. I mean, have you seen the statistics? Recent reports show that the global stone-coated product market is expected to grow at a solid 5.2% every year until 2028. That's pretty impressive, isn’t it? And it’s all thanks to folks wanting more durable and eco-friendly building options. Ultimate Checklist to Source the Best Stone Coated Products for Your Business One company really stepping up to the plate is Sengu (Shandong) New Materials Co., Ltd. They’re huge, covering almost 100 acres, and they’re not just about production—they’re all about blending research and development with sales. What’s really great is their focus on giving consumers stone-coated products that not only look good but also save them money on maintenance in the long run. In this blog, I’m going to give you the ultimate checklist for finding the best stone-coated products. This way, businesses can meet what consumers want while also sticking to their sustainability goals. Sounds good, right?
Key Trends in Stone Coated Product Technology for 2025

Looking ahead to 2025, we can already see some exciting trends in stone-coated product technology that are set to change the game for the industry. One major trend is the push for more sustainable manufacturing practices. With environmental issues becoming a hot topic, manufacturers are really getting into using eco-friendly materials and adopting energy-saving techniques. Not only does this resonate with consumers who care about the planet, but it also fits nicely with global regulations that aim to reduce carbon footprints.

Another cool development is the rise of smart technology in stone-coated products. You know how the Internet of Things (IoT) is creeping into different sectors? Well, now we have stone-coated products that come loaded with sensors! These bad boys can give real-time updates on performance and maintenance needs. It's a win-win: increased durability paired with lower maintenance costs make these products super appealing for businesses looking to save some bucks in the long run. By keeping up with these innovations, companies can make smarter sourcing choices and really sharpen their competitive edge in the market.

Stone Coated Products Technology Trends for 2025

Critical Factors for Evaluating Stone Coated Product Quality

So, when you're looking into stone-coated products for your business, quality should really be your top priority. First off, think about how durable the materials are. You want stone coatings that can handle tough weather, won’t rust, and keep their color over time. It’s a good idea to pick products that come with a warranty—it's often a sign that the manufacturer really believes in their durability.

Next up, don’t overlook the production process. Products made under strict manufacturing standards usually end up being of better quality. Try to find manufacturers who are open about how they source their materials and make their products. Knowing a bit about the production of these stone coatings can really help you understand how well they'll perform in the long run.

Oh, and here’s a quick tip: always ask for samples before you commit to a big order. This way, you can test them out yourself and make sure they meet your quality and performance expectations. Also, gathering reviews or case studies from other businesses that have successfully used these stone-coated products is a great way to check their reliability.

The Role of Sustainability in Modern Stone Coated Products

You know, sustainability is really becoming a big deal when it comes to making Stone Coated products. Businesses are starting to get more woke about their impact on the environment. Traditional materials like concrete? Yeah, they've definitely come under fire for their pretty hefty ecological footprint. That's why a lot of folks are on the lookout for alternatives that not only work well but are also kind to our planet. Stone coated products are a great example—they look like natural stone but are actually lighter and way more durable. Plus, they offer a sustainable choice that helps ease some of the negative effects tied to the usual building materials.

When you're on the hunt for the best stone coated products, think about weaving in some sustainable practices into your buying process. Try to find options made with recycled materials, or those that use cool production tech to cut down on waste and energy. And don't forget to choose suppliers who take sustainability seriously—it's crucial that their manufacturing vibes match up with eco-friendly values.

Oh, and just a little reminder: choosing stone coated products isn’t just about making things look good; it’s about making smart choices that show your business cares about the environment. By picking stuff that’s stylish and sustainable, you’re not just sprucing up your projects—you’re also helping to create a greener future. How cool is that?

Top Suppliers to Consider for Sourcing Stone Coated Products

When you're on the hunt for stone-coated products for your business, finding the right suppliers is super important to make sure you get quality and reliability. A few top suppliers to keep in mind are those manufacturers who really nail advanced coating technologies. You’ll want to look for companies that have a good reputation in the industry, plus some glowing customer reviews and certification standards that promise durability and performance.

Also, don’t forget to check out both local and international suppliers. Local folks might make logistics easier and be quicker to respond, while international suppliers could give you better pricing options. Take a good look at what they offer, their production capabilities, and how they handle after-sales support to find someone that fits your business just right. And hey, don’t be shy about asking for samples! Doing a solid comparison of materials can be a game-changer for your success in the market.

Ultimate Checklist to Source the Best Stone Coated Products for Your Business

How to Assess the Cost-Effectiveness of Stone Coated Solutions

Alright, so when businesses are looking at how cost-effective stone-coated products really are, they’ve got to think about more than just the sticker price. A report from the Roofing Industry Alliance for Progress points out that stone-coated roofs can actually save a ton of money in the long run. You see, these roofs can last for 50 years or even longer, which is pretty impressive compared to standard asphalt shingles that usually hang around for only 20 to 30 years. So, that longer lifespan means you won't have to worry about replacing them as often, plus you’ll spend less on maintenance over time.

Ultimate Checklist to Source the Best Stone Coated Products for Your Business

And let's not forget about energy efficiency because that's a huge piece of the puzzle. Research from the Oak Ridge National Laboratory shows that stone-coated materials are really good at reflecting solar heat, which can help lower those cooling bills during the summer months. Seriously, businesses could save up to 20% on energy costs each year, which definitely gives those profit margins a nice boost. So, when you invest in stone-coated products, you’re not just making your buildings look great and super durable—you're also reaping some solid financial benefits thanks to energy savings and lower lifecycle costs.

Innovative Applications of Stone Coated Products in Various Industries

You know, stone-coated products are really taking off in all kinds of industries these days, and it's all thanks to their incredible versatility and durability. I came across this market report from Grand View Research that says the global stone-coated roofing market is set to hit a whopping USD 2.81 billion by 2025, which is quite impressive with a growth rate of about 6.1% each year. A big part of this growth is the rising demand for sustainable and good-looking architectural options. You can see it everywhere—construction and landscaping guys are really embracing stone-coated materials because they can stand up to the weather and last for ages. So, they're perfect for roofs, siding, and other outdoor uses.

But it doesn’t stop there! The automotive world is also getting creative with stone-coated products, especially when it comes to car exteriors and some fancy accessories. Using these materials not only makes vehicles tougher, but it also helps them shed some weight, which is a big deal for better fuel efficiency. According to another report from Mordor Intelligence, the automotive coatings market is projected to soar to USD 28.3 billion by 2026, with stone-based coatings really stepping up as key players in the push for eco-friendly solutions. So whether we’re talking about homes or high-performance cars, stone-coated products are definitely making a name for themselves across so many different fields. It's cool to see how they’re becoming essential in modern manufacturing and design!

Ultimate Checklist to Source the Best Stone Coated Products for Your Business - Innovative Applications of Stone Coated Products in Various Industries

Industry Application Benefits Considerations
Construction Roofing Materials Durability, Aesthetic Appeal Weight, Installation Complexity
Manufacturing Decorative Panels Lightweight, Easy to Handle Cost of Production
Interior Design Wall Cladding Visual Appeal, Texture Variety Maintenance Requirements
Automotive Protective Coatings Corrosion Resistance, Weight Reduction Compatibility with Existing Materials
Energy Solar Panel Covers Enhanced Energy Efficiency, Durability Initial Investment Cost

Revamp Your Home's Aesthetic with Stone-Coated Metal Roofing Tiles: The Ultimate Guide to Architectural Elegance

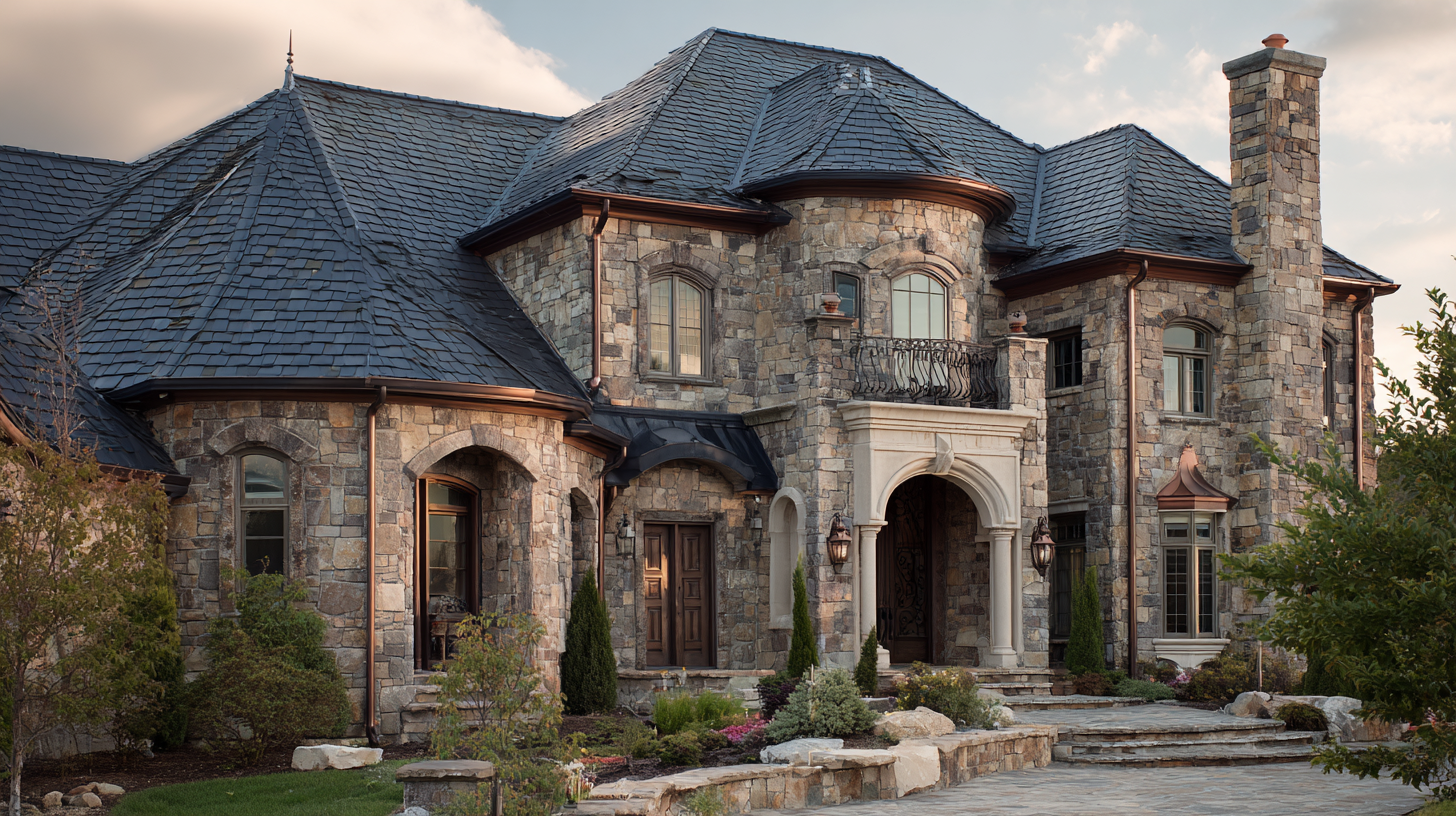
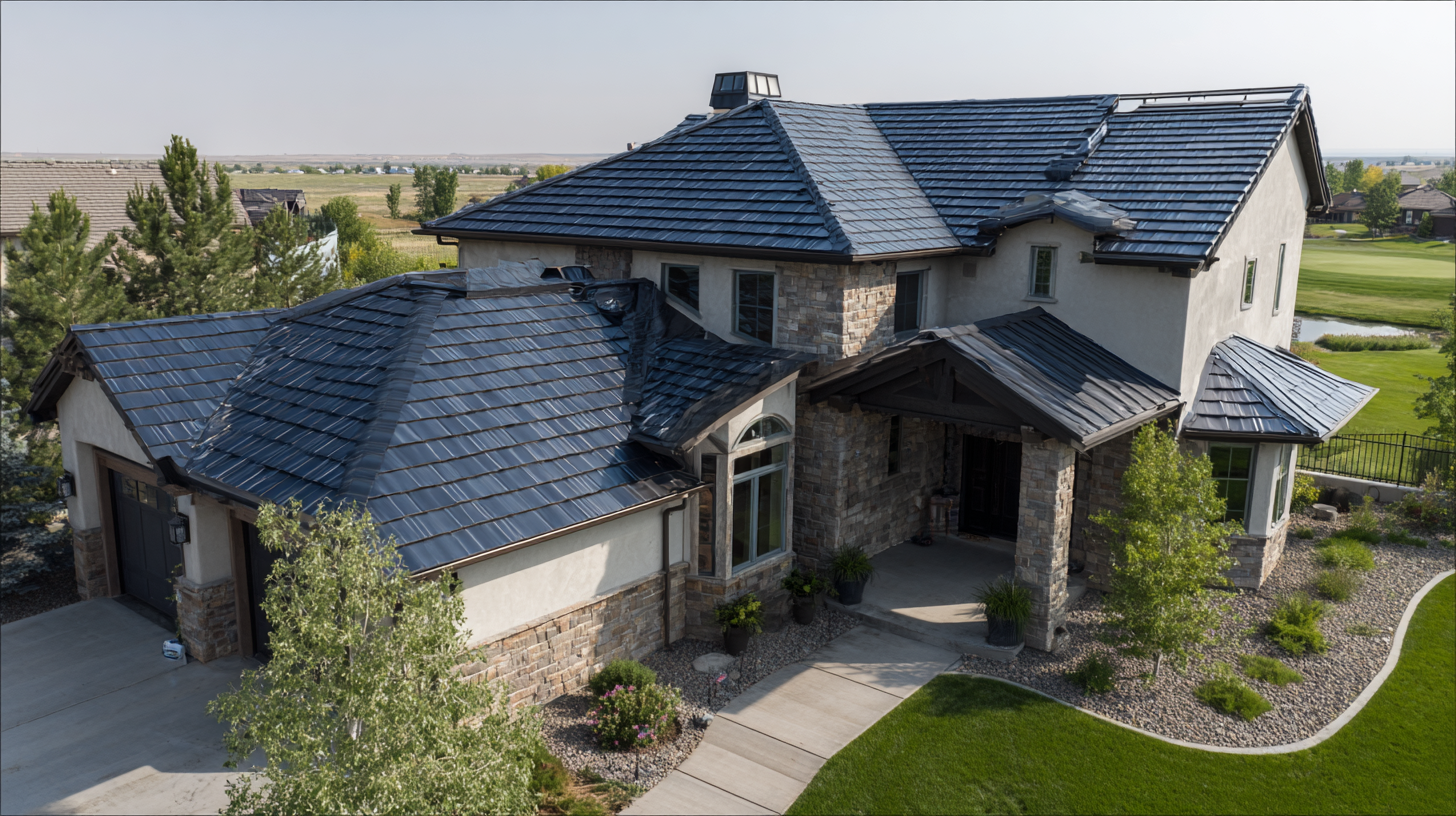
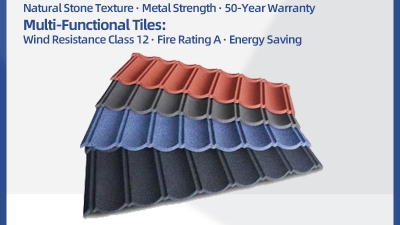
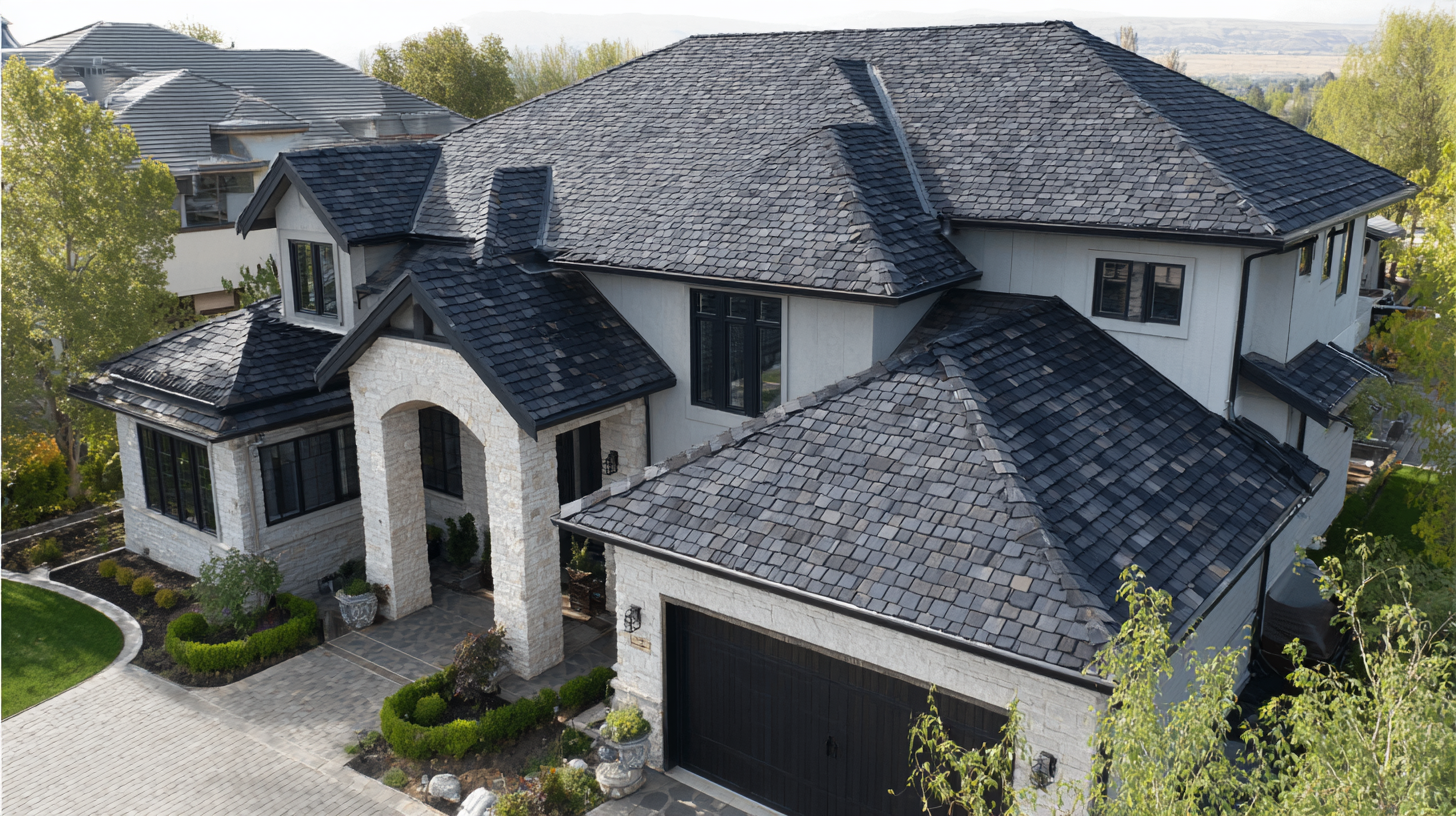
Revamping your home with Stone-Coated Metal Roofing tiles can significantly enhance its architectural elegance. Often overlooked, the roof serves as the "fifth façade" of a building; it plays a crucial role in defining the overall aesthetic appeal. By choosing stone-coated metal tiles, you transform what would typically be a functional element into a striking feature that captivates the eye. These tiles are not just durable but also come in a stunning variety of colors and textures, allowing homeowners to express their personal style while making a significant architectural statement.

The unique texture and finish of stone-coated metal roofing tiles create a visually appealing appearance that mimics traditional materials like slate or tile, yet with the added benefits of lightweight and resilience. This makes them an excellent choice for anyone looking to enhance the curb appeal of their home without compromising on durability or maintenance. Whether you aim for a classic look or a more contemporary design, these roofing tiles offer versatility that complements any architectural style, making your home not just stand out, but truly shine in its environment. Investing in stone-coated metal roofing is not only about aesthetics; it's also about creating a lasting impression that enhances the artistic landscape of your home.

FAQS

: What significant trend is emerging in stone-coated product technology for 2025?

: A key trend is the enhancement of sustainability in manufacturing processes, with a focus on eco-friendly materials and energy-efficient production techniques.

How is the integration of smart technology affecting stone-coated products?

Smart technology allows stone-coated products to be equipped with sensors that provide real-time data on performance and maintenance needs, increasing durability and lowering maintenance costs.

What lifespan can businesses expect from stone-coated roofs?

Stone-coated roofs typically have a lifespan of 50 years or more, significantly exceeding the 20-30 years lifespan of traditional asphalt shingles.

What are the primary financial benefits of stone-coated products?

They provide long-term savings through reduced replacement costs, lower maintenance expenses, and energy efficiency that can lead to annual savings of up to 20% in cooling costs.

How do stone-coated products contribute to energy efficiency?

Stone-coated solutions are effective at reflecting solar radiant heat, which helps lower cooling costs during hot months, contributing to overall energy savings.

Why is it important for companies to stay informed about advancements in stone-coated technology?

Staying informed enables companies to make informed sourcing decisions that enhance their competitive edge in the market by leveraging new technologies and sustainable practices.
Ethan

Ethan

Ethan is a dedicated marketing professional at Sengu (Shandong) New Materials Co., Ltd., where he leverages his extensive knowledge of the industry to drive the company's mission forward. With a passion for creating innovative home decoration solutions, he plays a crucial role in bridging the gap......
Previous 5 Essential Benefits of Choosing Stone Texture Wall Paint for Your Next Project